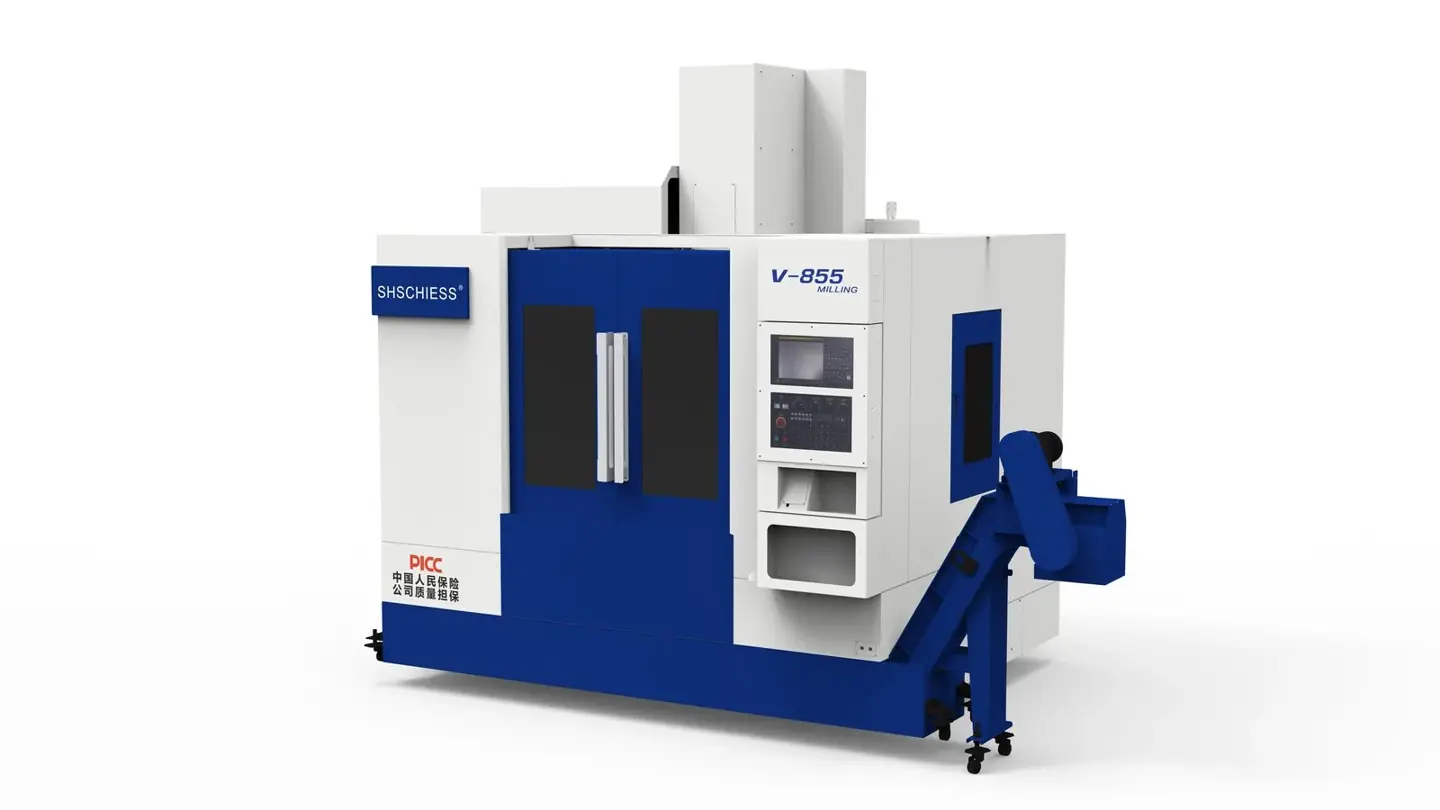
Representative series image. Configuration and enclosure may vary.
VERTICAL MACHINING CENTRES
V-855
The V-855 combines 800 × 550 × 550 mm X/Y/Z travel with a 1000 × 550 mm table for milling, drilling and pocketing. Review workpiece clearance and spindle options with our team.
Configured to order. Final specification, delivery and pricing are confirmed in your quotation.
TECHNICAL PROFILE
The details
that matter.
Reference configuration from manufacturer technical documentation. Options and document editions can differ; agree the exact configuration before ordering.
| Parameter | Specification | Unit |
|---|---|---|
| X-axis travel | 800 | mm |
| Y-axis travel | 550 | mm |
| Z-axis travel | 550 | mm |
| Table size | 1000 × 550 | mm |
| Table load | 600 | kg |
| Spindle taper | BT-40 | |
| Spindle speed | 10000 | rpm |
| Spindle motor | 7.5 | kW |
| Spindle nose to table | 120-670 | mm |
| Spindle centre to column | 595 | mm |
| Rapid traverse X/Y/Z | 48/48/48 | m/min |
| Positioning accuracy (full travel) | ±0.006 | mm |
| Repeatability (full travel) | ±0.004 | mm |
| Tool magazine capacity | 24 | |
| Maximum tool length | 300 | mm |
| Maximum tool weight | 8 | kg |
| Tool holder | BT40 | |
| Power requirement | 25 | kVA |
| Machine weight | 5000 | kg |
| Machine dimensions (L × W × H) | 2700x2500x2800 | mm |
FROM SPECIFICATION TO PRODUCTION
Let your component
lead the conversation.
Share the workpiece
Send material, dimensions, drawings and your required tolerances.
Define the process
Review workholding, tooling, spindle speed and control requirements.
Confirm the configuration
Agree a technical proposal, acceptance criteria and delivery schedule.
CONFIGURATION IN CONTEXT
Planning with V-855.
Fit the fixture, not just the part
X/Y/Z travel defines axis movement. Table dimensions, allowable load, spindle-to-table clearance and tool length determine how the workpiece and fixture fit in practice.
Choose the spindle and tools together
Confirm tool interface, speed, torque requirements and magazine capacity. A catalogue speed option is not automatically supplied; the controller and spindle package belong in the technical agreement.
Plan inspection before production
Identify datum surfaces, critical bores, tolerances and the measurement method. Agree a representative sample and acceptance sequence before treating a travel envelope as proof of production capability.
V-855 or V-1160?
These are published differences between the reference configurations. They help narrow a shortlist; they do not establish interchangeable tooling or identical performance.
| Parameter | V-855 | V-1160 |
|---|---|---|
| X-axis travel | 800 mm | 1100 mm |
| Y-axis travel | 550 mm | 600 mm |
| Z-axis travel | 550 mm | 600 mm |
| Table size | 1000 × 550 mm | 1200 × 600 mm |
PRACTICAL ANSWERS
V-855 FAQ
What is the x-axis travel of V-855?
V-855 lists 800 mm for x-axis travel in the reference configuration. Confirm this value in the order-specific technical agreement and check tooling and workholding clearance.
What is the y-axis travel of V-855?
V-855 lists 550 mm for y-axis travel in the reference configuration. Confirm this value in the order-specific technical agreement and check tooling and workholding clearance.
What is the z-axis travel of V-855?
V-855 lists 550 mm for z-axis travel in the reference configuration. Confirm this value in the order-specific technical agreement and check tooling and workholding clearance.
What should I compare with V-855?
V-1160 is another model in this machine family. Review the differences above and both specification tables against the same drawing, tooling and installation requirements.
What is the price and delivery time for V-855?
This machine is configured to order. Send your controller preference, workpiece details, accessories and delivery destination so the team can confirm a complete quotation and production schedule.
How will V-855 be inspected before acceptance?
Agree the supplied configuration, geometric checks, sample machining and measurement method before ordering. Factory pre-acceptance and acceptance after installation should use the agreed technical requirements. See our quality and acceptance guide for the inspection planning process.
YOUR NEXT PRODUCTION CHAPTER
Let’s build what
comes next.
Start with your component, material and production target. We will help define the machine configuration.
Discuss your project